 You are here:
Auto-Feed Riveting Gun Operation and Maintenance FAQ
How well a machine performs after installation depends half on selection and half on how it is operated and maintained. This guide collects what the shop floor needs to know about an auto-feed riveting gun: how it is built, how to run it, what to watch during continuous shifts, the maintenance schedule, and how to clear common faults. Shop-floor supervisors and operators can follow it directly. The points below are general; the manual shipped with the machine and the on-site training take precedence.
For distributors and contract manufacturers, a single supplier with a full range shortens the purchasing cycle. The notes below cover auto-feed riveting gun supply and procurement.
In short, for buyers who source machines, rivets and spare parts in one order: structure and design logic of an auto-feed riveting gun; standard operating procedure (step by step for new operators); how does a pneumatic high-force automatic rivet gun set rivets so fast?; what to watch during continuous operation.
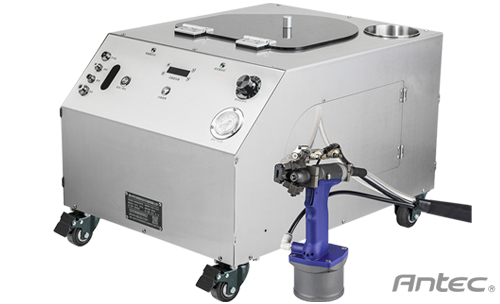
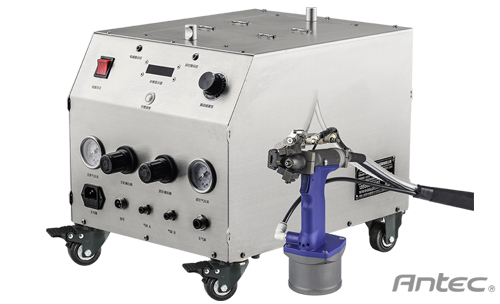
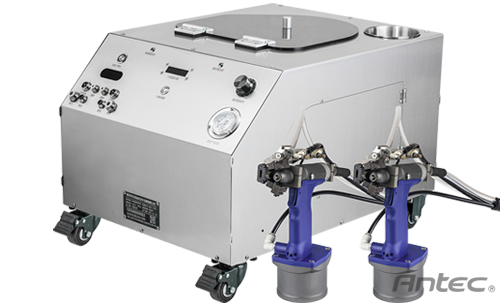
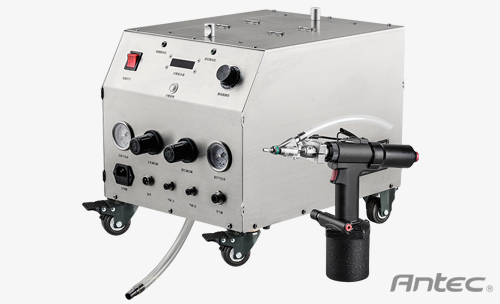
1. Structure and Design Logic of an Auto-Feed Riveting Gun
| Module | Function | Maintenance focus |
|---|---|---|
| Vibratory bowl / hopper | Sorts, orients and separates rivets | Clean bowl; no deformed rivets mixed in |
| Blow-feed system (feed tube) | Compressed air carries rivets to the nosepiece | Stable air pressure; no kinks or leaks in the line |
| Rivet gun body | Clamps the rivet, pulls it and breaks the mandrel | Wear on the nosepiece, jaws and anvil |
| Control box | Parameters, counting, alarms | Sensor signals and secure wiring |
| Workbench / fixture | Workpiece location (fixed version) | Locating pins and clamps stay tight |
The design logic is simple: the main unit has to deliver the right rivet on time, and the gun body has to break it cleanly. That is why jam and no-feed faults are traced through the feed path first, while weak pull force starts with air pressure and worn gun parts. Splitting the machine into stages finds the cause fastest.
2. Standard Operating Procedure (Step by Step for New Operators)
Step 1: connect air and power and confirm the air pressure is inside the range given in the manual. Step 2: empty any rivets left in the bowl, then load rivets that match the nosepiece; do not overfill. Step 3: run a few dry cycles and listen to the rhythm of separation, blow-feed and mandrel break. Step 4: clamp the workpiece, press the nosepiece square to the hole and pull the trigger; move the gun only after the mandrel breaks. Step 5: at the end of the shift, empty the remaining rivets, clean the nosepiece, and shut off air and power. Antec installs, commissions and trains on site at delivery, and a new operator is productive after a short training session because the operation itself is not difficult. For details, see is an auto-feed riveting gun hard to operate? Onboarding and training.
Specification customization is quoted with the machine, not as a separate negotiation.
3. How Does a Pneumatic High-Force Automatic Rivet Gun Set Rivets So Fast?
Speed comes from three stages that run in parallel and are compressed to a minimum. First, the machine sorts and feeds rivets automatically, which removes manual rivet loading, the slowest step in hand riveting. Second, compressed air blows each rivet to the nosepiece with almost no waiting. Third, one trigger pull completes pull, set and mandrel break at a cycle time of about 70 cycles/min. The operator only positions the tool and pulls the trigger, and one machine replaces the repetitive work of about 3 riveters. Real output also includes pick-and-place and repositioning time, so time a complete part rather than a single rivet. The method is in how many rivets per minute, and how to calculate capacity.
4. What to Watch During Continuous Operation
1) Secure the air supply. High cycle rates draw a lot of air, and an undersized compressor or air receiver makes the gun weaker as the shift goes on, so size the pump to the manual and drain the water traps regularly. 2) Top up the bowl in good time to avoid dry cycles, and pull out deformed or burred rivets instead of letting them back into the feed. 3) Stop and check if the nosepiece gets hot or the gun starts to sound wrong; do not keep running a machine that is already complaining. 4) Clean the rivet inlet on the nosepiece and check the jaws about every 2 hours. 5) On two-shift lines, keep nosepieces and jaws in stock as wear parts to hold unplanned downtime to a minimum.
Consumables ordered with the equipment avoid a second shipment later.
5. Daily Checks and Maintenance (Daily / Weekly / Monthly)
| Interval | Checks |
|---|---|
| Before the shift | Air pressure, clean nosepiece and jaws, dry feed run, air line fittings for leaks |
| After the shift | Empty remaining rivets, wipe the nosepiece and rivet inlet, shut off air and power, coil the feed tube |
| Weekly | Lubricate moving parts as the manual specifies, clean the vibratory bowl, wipe the sensors |
| Monthly | Check wear on nosepiece, jaws and anvil, tighten screws, check wiring and alarm functions |
Use the oil and wear-part specifications in the manual, and do not substitute oil grades or fit non-matching nosepieces. Wear parts can be ordered from the factory at cost. For the full maintenance checklist and fault prevention see how to maintain an auto-feed riveting gun day to day, and for repair and parts service see auto-feed riveting gun repair, maintenance and parts supply.
6. Common Faults and How to Fix Them
| Symptom | Common causes | Fix |
|---|---|---|
| Jammed or no rivet feed | Deformed rivet, blocked or dirty track, wrong nosepiece size | Stop the machine, clear the track, remove bad rivets, fit the matching nosepiece |
| Mandrel will not break | Low air pressure, worn or slipping jaws, nosepiece not seated | Adjust air pressure, replace the jaws, correct the seating technique |
| Weak pull or loose joint | Insufficient pressure, leaking air line, worn anvil | Find and fix the leak, restore pressure, replace worn parts, verify pull force |
| Air leak or abnormal noise | Aged seals, loose fittings | Replace seals, tighten or replace fittings |
| Counting or alarm errors | Dirty or displaced sensors, loose wiring | Clean the sensors, reseat them, check the wiring |
| Scratched workpiece | Nosepiece impact, poor square alignment | Replace the nosepiece, reinforce operator training, locate parts with a fixture |
If the same position jams repeatedly or pull force stays abnormal, stop the machine, keep a video of the fault and call service before anything else; small problems left alone turn into a damaged gun body. For whether you can keep your existing gun, and where main unit and gun compatibility ends, see can an auto-feed riveting gun use my own high-force automatic rivet gun; for machining accuracy, and roughing and finishing notes, see how to guarantee machining accuracy on an auto-feed riveting gun.
Operation and Maintenance FAQ
Common Questions on Operation and Care
Q1: How soon can we go into full production after the machine arrives?
Installation, commissioning and training are normally completed the same day. Once a loaded trial on your actual parts confirms cycle time and yield, you can start production; non-standard models depend on the on-site integration.
Q2: Our operators turn over quickly. What happens when someone new takes over?
The machine has a low operating threshold. Train internally with this guide and the manual, or ask the factory for a refresher training session or remote guidance.
Q3: How often should nosepieces and jaws be replaced?
There is no fixed number of days; it depends on rivet material, daily output and how thoroughly the machine is maintained. Replace them when inspection shows wear beyond limits, and keep 1-2 spare sets on high-cycle lines.
Q4: Can the machine run 24 hours continuously?
The design supports long continuous runs, provided the air supply is stable and cleaning and wear-part checks are done during the shift. The rated continuous duty for a specific model is stated in its manual.
Global Customers: Fault Response and On-Site Maintenance
We provide on-site repair, maintenance training and genuine factory parts to customers worldwide. Call +86 13556668682.
Further reading: maintenance tasks, intervals and fault prevention for auto-feed riveting guns · how to calculate riveting cycle time and capacity · auto-feed riveting gun selection advice
Auto-Feed Riveting Gun at a glance: 20,000 N pull force, 70 rivets per minute, bulk orders shipped worldwide, one-stop supply of machines, rivets and parts.
Bulk orders are packed and shipped together, with technical support included.
One supplier for the whole riveting process
Tell us what you buy today and in what volume. We will consolidate the machines, the consumables and the parts into one offer.
 Previous