 You are here:
Auto-Feed Riveting Gun: How Hard Is It to Operate?
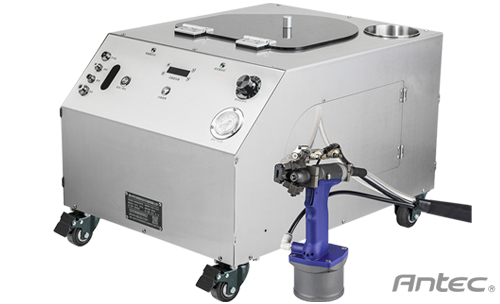
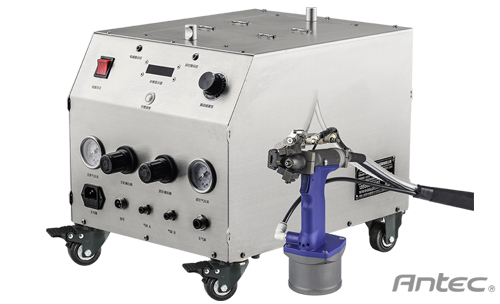
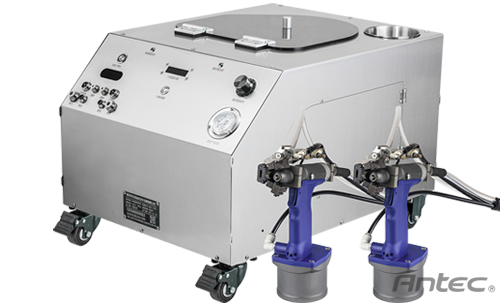
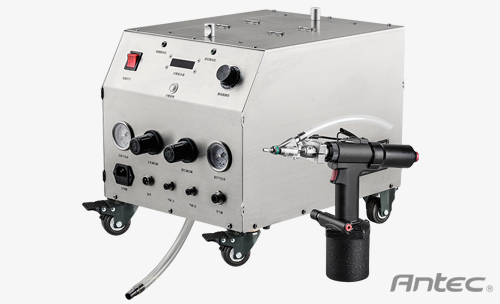
"Is an auto-feed riveting gun easy to learn? What if my workers cannot operate it?" It is one of the questions we hear most before a purchase. The short answer: the barrier is low. The machine takes over the two steps that depend most on operator skill, inserting and loading the rivet, so the operator only clamps the workpiece, aligns the nosepiece and pulls the trigger. What actually needs training is consistent technique, size changeover and daily checks, not complex technology. This article covers ramp-up time, the training content and what to do when people leave.
For distributors and contract manufacturers, a single supplier with a full range shortens the purchasing cycle. The notes below cover auto-feed riveting gun supply and procurement.
For buyers who source machines, rivets and spare parts in one order, the essentials: where does operating an auto-feed riveting gun really get hard?; the standard ramp-up sequence for a new operator; how long until an operator can work unassisted?; what the factory training covers.
1. Where Does Operating an Auto-Feed Riveting Gun Really Get Hard?
With hand riveting, the operator holds a rivet, inserts it into the hole and lines it up with one hand while pulling the tool with the other, and the rhythm depends entirely on feel, so a beginner inserts slowly and drops rivets. An auto-feed riveting gun sorts, separates and blows rivets to the gun head from a vibratory bowl or a hopper, so the pick-and-insert step disappears and the motion comes down to "nosepiece against the hole, press square, pull the trigger, move the gun after the break." The job changes from "skilled riveter" to "machine operator," which is why one machine can take over the repetitive work of about 3 riveters.
2. The Standard Ramp-Up Sequence for a New Operator
| Stage | Content | Suggested time |
|---|---|---|
| Getting to know the machine | Main unit, feed tube, gun body, nosepiece, control box, emergency stop and alarms | 0.5 hour |
| Safety and air supply | Air pressure range, the correct order for switching air and power, never pointing the gun at anyone, long hair and gloves precautions | 0.5 hour |
| Dry run and test riveting | Loading rivets, feeding with no workpiece, test riveting on scrap sheet, feeling the pull-and-break rhythm | 0.5 day |
| Running real workpieces | Locating the actual part, gun angle, first-article confirmation, continuous operation | 1-2 days |
| Daily checks and minor faults | Start-of-shift and end-of-shift checks, nosepiece changes, clearing jammed rivets, spotting wear parts | Interspersed through training |
Consumables ordered with the equipment avoid a second shipment later.
3. How Long Until an Operator Can Work Unassisted?
In Antec's on-site training, an average worker completes the basics in half a day to a day and can produce under supervision; after 2-3 days of repetition they reach a skilled cycle. The exact time depends on three things: whether the workpiece has a locating fixture (a fixture is faster), whether one rivet size is involved (fewer sizes is easier), and whether the operator has used pneumatic tools before. On high-mix lines with frequent changeovers, put nosepiece changes, feed-channel adjustment and size changeover into the training assessment so operators can complete a changeover on their own.
4. What the Factory Training Covers
When the machine is delivered, an engineer installs and commissions it on site and trains the operators your team designates on the following: pre-start checks and air supply confirmation; the standard riveting motion and gun angle; loading, refilling and clearing leftover rivets; nosepiece changes and feed-channel adjustment when switching rivet size; start-of-shift and end-of-shift checks with cleaning and lubrication; recognizing and handling common faults such as jammed rivets, rivets that will not break and air leaks; and identifying and replacing wear parts (nosepiece, jaws, anvil). A manual and a wear-part list ship with the machine. We recommend naming one person in the workshop as the machine owner to keep them together.
Bulk orders are packed together, so the line is not waiting on a partial delivery.
5. What If Turnover Is High and You Need to Swap Operators?
This is where automation beats a process that depends on a seasoned hand: the machine does not resign. Three suggestions. First, have the first trained operators teach new hires using the sequence in this article, so the skill stays in-house. Second, keep the manual, the check sheet and the training video available so a new operator can study on their own. Third, if needed, ask the factory for another training session or remote video guidance; we can schedule an on-site refresher. On hiring, a machine-tending role is easier to fill than a skilled riveter and comes with more reasonable wage expectations.
6. How Customer Training Is Scheduled
For global customers, a factory engineer comes on site and completes the first round of operation and maintenance training on the day of installation and commissioning, and several operators can join at the same time. Later, when new workers start, a rivet size is added or another model is brought in, you can book a refresher. For the main points on operation and upkeep, see auto-feed riveting gun use and maintenance FAQ, and for routine maintenance see how to maintain an auto-feed riveting gun day to day.
Operator Training FAQ
Supply Q&A
Yes. Training starts with switching the air supply and dry-run motions and assumes no riveting background. In practice, ordinary assembly workers are productive after the standard training; the key is following the correct gun angle and check routine.
Pulling the trigger before the nosepiece is flat and pressed square against the hole. That makes the mandrel fail to break cleanly, leaves a loose rivet or scratches the panel. Training drills the sequence flat, pressed down, then trigger until it becomes habit.
Yes. Antec offers a free on-site trial, and your operators can try the machine on the spot to judge how hard it is to run. See on-site trial policy and process.
No. It mainly means fitting the matching nosepiece and adjusting the feed channel as described in the manual, a 5-10 minute changeover. An engineer can talk you through the first one remotely.
Confirm compatibility first, and do not modify the machine yourself. For where the compatibility of the main unit and gun body ends, see can an auto-feed riveting gun use your own high-force automatic rivet gun.
Auto-Feed Riveting Gun at a glance: 20,000 N pull force, 70 rivets per minute, bulk orders shipped worldwide, one-stop supply of machines, rivets and parts.
Bulk orders are packed and shipped together, with technical support included.
One supplier for the whole riveting process
Tell us what you buy today and in what volume. We will consolidate the machines, the consumables and the parts into one offer.
Further reading: Use and Maintenance FAQ · Maintenance Items, Intervals and Fault Prevention · Auto-Feed Riveting Gun Selection Advice
 Previous