 You are here:
Auto-Feed Riveting Gun Cycle Time: Rivets per Minute and Capacity
How Many Rivets per Minute Can an Auto-Feed Riveting Gun Set? Cycle Time and Capacity Math
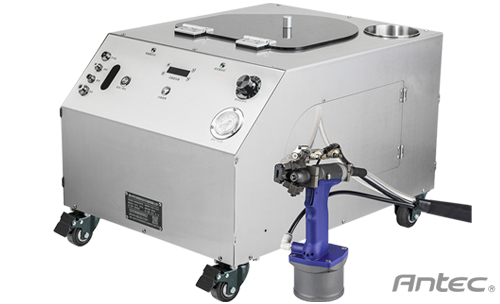
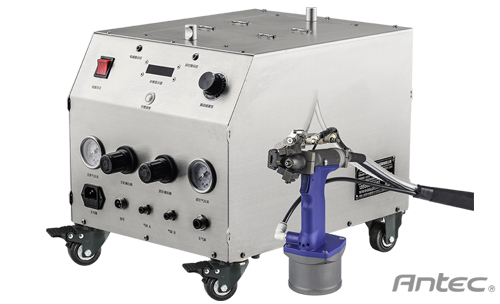
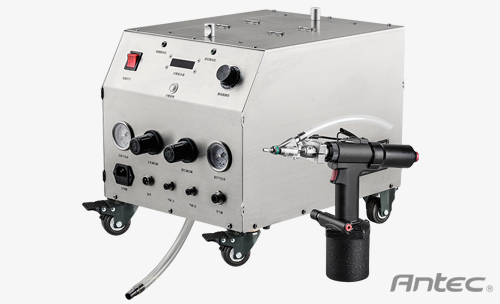
"How many rivets per minute can an auto-feed riveting gun set?" is one of the questions we hear most often. Under standard conditions a typical Antec machine runs at about 70 rivets per minute, which works out to roughly 4,800 rivet points per hour in theory. That figure describes continuous machine motion, though. On a real product you still have to subtract loading and unloading, repositioning, and changeover time. This article shows how to calculate true output and which factors slow the cycle down.
One order covers the equipment and the consumables, so the line does not stop waiting for a second shipment. The notes below cover auto-feed riveting gun supply and procurement.
What buyers who source machines, rivets and spare parts in one order should remember: rated cycle time vs. real output; four factors that affect speed; how much faster than hand riveting?; base capacity decisions on trial data.
1. Rated Cycle Time vs. Real Output
Rated cycle time covers one complete "feed, insert, set, retract" sequence: about 0.7-0.8 seconds per rivet, or roughly 70 rivets per minute. Real time per part also includes loading, unloading, flipping the workpiece, and moving between rivet points. Capacity should therefore be based on a measured cycle for one complete part, not on 80 multiplied by the number of working minutes.
| Basis | Value (reference) | Notes |
|---|---|---|
| Single rivet cycle | About 0.7-0.8 seconds per rivet (about 70 rivets per minute) | Standard rivet, standard feed distance |
| Theoretical rivet points per hour | About 4,800 points | Excludes loading, unloading and repositioning |
| Actual effective output | Based on on-site measurement | Includes part handling, flipping and changeover time |
| Dual-gun, two rivets per cycle | Two guns in parallel, close to double the output | Best for standardized housings with dense rivet patterns |
Price per rivet, not price per machine, is the number that survives the first year.
2. Four Factors That Affect Speed
Rivet size and type. Longer rivets and larger head diameters take longer to sort and feed. Stainless steel and structural rivets need a longer setting stroke, which adds time to every rivet.
Feed distance and hose routing. The distance from the machine to the gun, the hose length, and how sharply the hose bends all affect how long each rivet takes to arrive. Keep the hose short and avoid tight bends when you lay out the workstation.
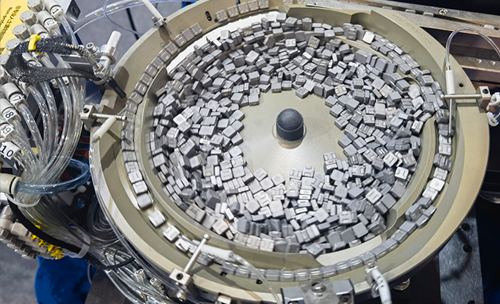
Machine configuration. A handheld gun is limited by how fast the operator can move. Fixture-mounted or fixed-station models deliver the most consistent results. A dual-gun machine runs two guns in parallel and suits parts with two rows of rivet points that can be set at the same time. A robotic cell holds a steady cycle and can run unattended.
Feed reliability. Jammed or missed rivets mean stoppages and rework, so real efficiency depends on sustainable speed rather than peak speed. Antec machines refill automatically and correct rivet orientation on their own; in continuous testing they ran 30,000 cycles without a jam, and the long-term failure rate is about 0.3%.
3. How Much Faster Than Hand Riveting?
Hand riveting means picking up a rivet, inserting it, aligning the hole, and then pulling the tool - several seconds per rivet, with quality that varies from one operator to the next. On an automatic machine the feed system delivers the rivet straight to the nosepiece, so the operator only positions the part and pulls the trigger. One machine replaces about 3 riveting workers and can lift overall efficiency by up to 3x. More important, the cycle stays consistent: output no longer depends on skilled or temporary labor, so peak-season capacity becomes predictable.
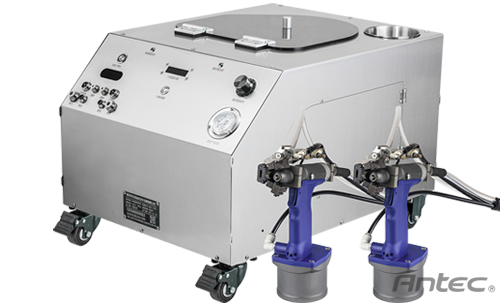
Original parts keep the wear rate predictable across a fleet of units.
4. Base Capacity Decisions on Trial Data
At the line-planning stage, estimate time per part by dividing the number of rivet points by the measured cycle time and then adding handling time; combine that with your shift pattern to size daily output and the number of machines you need. Antec can bring a machine to your plant, time it with your own rivets and workpieces, and report cycle time per rivet, time per part, and yield. The proposal and quotation are built on those figures, so you never plan a line around a brochure peak number.
5. How to Measure Cycle Time and Capacity on the Floor
Planning a line around a brochure peak speed is a quick way to miss your target. Measure it the way described below during a machine trial; the figures feed straight into machine count and payback calculations:
| What to measure | Method |
|---|---|
| Cycle time per rivet | Set 50-100 rivets continuously, divide total time by the number of rivets, and take the average |
| Time per part | Actual time to finish one complete part, including loading, unloading, flipping and repositioning |
| Yield | Count missed rivets, stripped threads, scratches, and rivets whose mandrel does not break, as a share of the total |
| Operating rate | Actual run time as a share of shift time, after deducting changeover, refilling and breaks |
| Daily output | Shift length multiplied by operating rate, divided by time per part, plus a reasonable allowance |
Time the same part twice - once with a skilled operator working by hand, once on the automatic machine - and compare time per part and yield. If a dual-gun option is on the table, run a third set with both guns to see the real gain on that part. During an on-site trial, Antec records these figures and puts the conclusions in writing as the basis for the proposal and quotation.
Common Questions About Cycle Time
Buyer Questions
70 rivets per minute is a reference value for one riveting cycle. Real output includes loading, unloading and repositioning, and larger rivets or widely spaced rivet points add time per part. That is normal.
On parts with two symmetrical rows of closely spaced rivet points, two guns come close to doubling output. If the points are scattered or the part has to be repositioned often, the gain shrinks. Test both setups on your own part.
The advantage of a robot is a steady cycle and unattended continuous operation, which suits high-volume parts with fixed rivet points. For high-mix, low-volume work, a handheld or fixed-station machine is more flexible and more economical.
Quoted figures are usually the ideal time for a single cycle. The real gap comes from feed reliability (jams and stoppages), changeover time, and how well the operator and machine work together. Timing a complete part during a trial tells you far more than a per-rivet number.
Auto-Feed Riveting Gun at a glance: 20,000 N pull force, 70 rivets per minute, bulk orders shipped worldwide, one-stop supply of machines, rivets and parts.
Consumables and wear parts are quoted alongside the machine, so the total cost per rivet is visible before the order.
Machines, rivets and parts in one order
Send the equipment list and the annual rivet consumption. We will quote the package, the bulk price and the shipping in one reply.
Further reading: Auto-Feed Riveting Gun Buying Guide (full series) · Automation for Sheet Metal and Stainless Steel Fabrication · Auto-Feed Riveting Gun Product Center
 Previous