 You are here:
Rivet Nut vs Self-Clinching Nut: Appliance and Cabinet Guide - Procurement
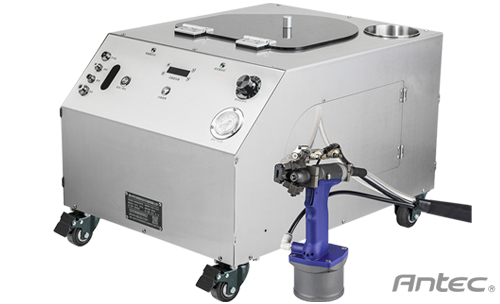
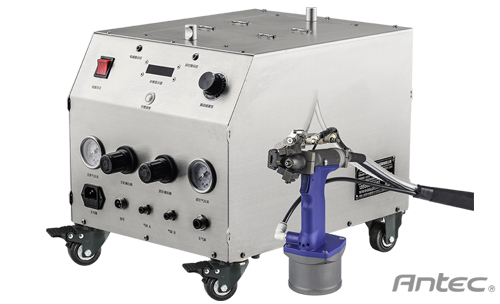
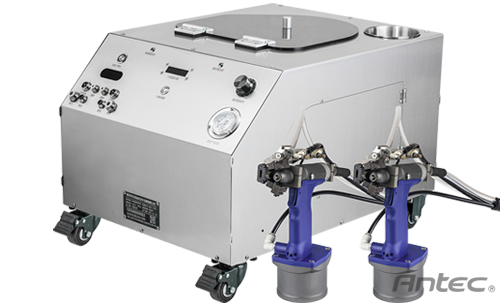
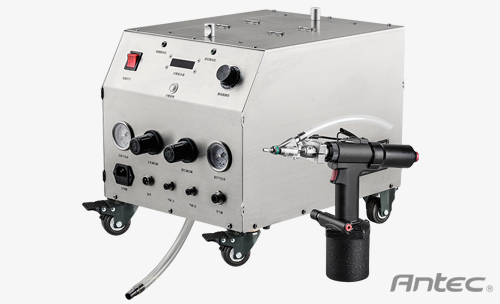
Appliance and cabinet shops keep coming back to the same question on thin sheet: rivet nut or self-clinching nut? Both create an internal thread in a thin panel, but the process, the equipment and the best use case differ sharply. Here is how they compare on the shop floor, and where a high-force rivet nut gun earns its place.
One order covers the equipment and the consumables, so the line does not stop waiting for a second shipment. The notes below cover high-force rivet nut gun supply and procurement.
What buyers who source machines, rivets and spare parts in one order should remember: how the two processes differ; how to choose on the shop floor; sizing guidance; trial the high-force rivet nut gun, then fix the process.
1. How the Two Processes Differ
| Item | Rivet nut | Self-clinching nut |
|---|---|---|
| Forming method | Axial pull and cold forming with a high-force rivet nut gun | Radial press-in with a clinching press or punch press |
| Equipment | Handheld or high-force rivet nut gun, flexible | Needs a clinching press or die set, fixed station |
| Sheet thickness | Friendly to thin sheet, aluminum extrusion and irregular parts | Demanding on sheet thickness and hole consistency |
| Rework on site | Can be re-fitted in place after powder coating | Hard to rework once pressed wrong, needs dedicated equipment |
| Typical use | Cabinet doors, appliance panels, pallets | High-volume standard flat panels, pre-assembled chassis parts |
2. How to Choose on the Shop Floor
Appliances and kitchen equipment mean many variants, irregular parts and a lot of rework after powder coating, which suits the flexible rivet nut. Aluminum extrusion, battery trays and energy storage cabinets, meaning any structure that gets taken apart for service, also favor rivet nuts. For high-volume standard flat panels pre-assembled on a die-based line, the self-clinching nut is faster. Many plants run both: clinch the standard parts, rivet the irregular ones and the rework.
Price per rivet, not price per machine, is the number that survives the first year.
3. Sizing Guidance
M3-M6 covers appliance thin-sheet panels, M6-M10 covers cabinet doors and mounting plates, and M10-M12 covers aluminum extrusion beams and trays; on aluminum parts use a knurled rivet nut rated for aluminum and verify with a pull-out test. Appliance solutions are on our appliance, kitchen and hardware furniture riveting page, cabinet solutions on the power distribution cabinet and electrical equipment page.
4. Trial the High-Force Rivet Nut Gun, Then Fix the Process
When you are not sure, hand the part and the sheet thickness to an engineer and run one sample set with riveting and one with clinching, then compare forming, pull-out strength, appearance and rework cost before deciding. Antec can run a rivet nut sample at your plant; for general background see high-force rivet nut gun product overview.
Buyer Questions
Aluminum extrusion, irregular parts and structures that get disassembled usually favor the rivet nut; clinching is more demanding on the profile and the press, so confirm with a side-by-side trial.
Set a rivet nut into the prepared hole right through the coated part; it takes a few minutes and does not damage the finish.
High-Force Rivet Nut Gun at a glance: 20,000 N pull force, 70 rivets per minute, bulk orders shipped worldwide, one-stop supply of machines, rivets and parts.
Consumables and wear parts are quoted alongside the machine, so the total cost per rivet is visible before the order.
Machines, rivets and parts in one order
Send the equipment list and the annual rivet consumption. We will quote the package, the bulk price and the shipping in one reply.
 Previous